Two-Shot ist ein praxisnahes ingenieurwissenschaftliches Thema, wenn man verschiedene Optionen vergleichen, Grenzwerte prüfen und einen Prozess mit geringerem Risiko auswählen muss.
Multi-Material Molding Overview

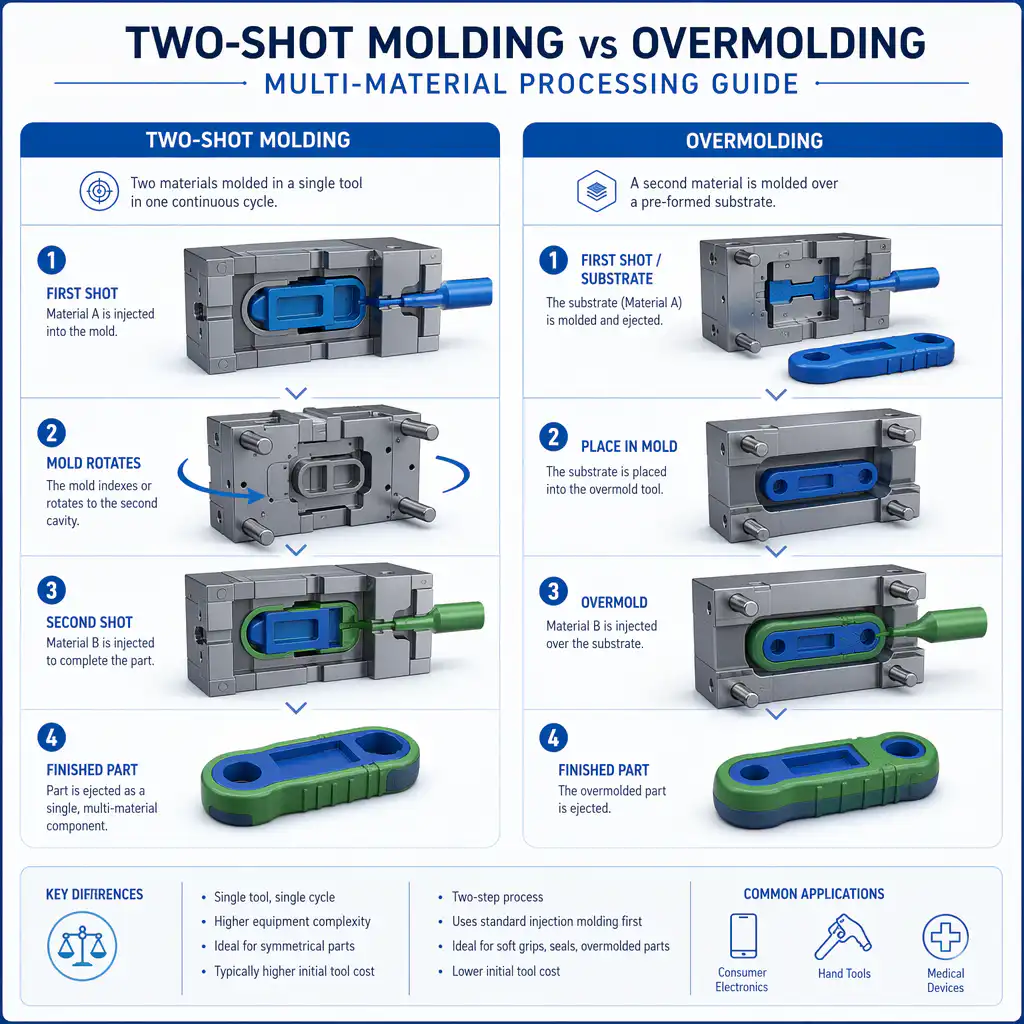
Multi-material molding combines different materials in a single part to achieve functional or aesthetic benefits. Two-shot molding and overmolding are the primary techniques, each with distinct advantages.
Two-Shot Molding
Two-shot molding (also called 2K molding or multi-component molding) injects two different materials in a single molding cycle using a specialized machine with two injection units.
Prozessbeschreibung
- First material injected into mold cavity
- Mold rotates or transfers to second position
- Second material injected over or alongside first
- Part ejected as complete unit
Vorteile
- Excellent material bonding (chemical bond possible)
- High precision and repeatability
- Single cycle production
- Design flexibility for complex geometries
- Reduced labor and handling
Nachteile
- Higher machine and tooling cost
- Requires specialized equipment
- Less flexibility for design changes
- Longer tooling lead time
Umspritzen
Overmolding uses two separate molding cycles. A substrate part is molded first, then placed in a second mold where additional material is injected over it.
Prozessbeschreibung
- Substrate molded in first mold
- Substrate placed in second mold
- Second material injected over substrate
- Completed part ejected
Vorteile
- Lower equipment cost
- Can use standard injection machines
- More design flexibility
- Easier to change colors/materials
- Suitable for lower volumes
Nachteile
- Requires two molding cycles
- Additional handling and labor
- Bond quality depends on mechanical interlock
- Higher per-part cost at high volumes
Material Compatibility
Anwendungen
Two-Shot Molding:
- Automotive interior components
- Medical devices with soft grips
- Consumer electronics buttons and keys
- Sealed enclosures with gaskets
Overmolding:
- Tool handles and grips
- Encapsulated electronics
- Cable connectors
- Product branding and logos
Decision Factors
- Volume: High volume favors two-shot; low volume favors overmolding
- Bond requirements: Chemical bond needs two-shot
- Budget: Overmolding has lower upfront costs
- Ausrüstung: Two-shot requires specialized machines
Schlussfolgerung
Both techniques produce multi-material parts successfully. Evaluate production volume, bond requirements, and available equipment to determine the best approach.
Process Decision Table for Production Parts
| Entscheidungsfaktor | Two-shot molding | Umspritzen |
|---|---|---|
| Tooling route | One indexed or rotary tool with two injection units | Separate substrate and overmold steps, or an insert tool |
| Optimale Passform | High registration, repeatability and production volume | Flexible launches, inserts or lower initial tool complexity |
| Hauptrisiko | Transfer alignment, shot balance and interface validation | Insert position, surface preparation and bond variation |
| Validation | Registration, weld lines and interface strength | Retention features, cleanliness and pull testing |
Choose after checking the material pair, annual volume, gate and parting-line limits, substrate tolerance and the test method for the completed interface. Include the DFM drawing, material datasheets, trial plan and bond requirement in the RFQ. See the overmolding guide for the broader tooling route.
FAQ
When does Two-Shot Molding vs Overmolding — Multi-Material Processing Guide make sense?
Two-Shot Molding vs Overmolding — Multi-Material Processing Guide makes sense when the part volume, material choice, geometry, and repeatability needs justify mold design and tooling investment.
What design factors matter most for Two-Shot Molding vs Overmolding — Multi-Material Processing Guide?
Wandstärke, Rippen, Vorsprünge, Entformungsschräge, Angussposition, Schrumpfung, Trennfuge und Auswurf – all diese Faktoren beeinflussen die Qualität des Formteils.
Welche Informationen werden vor der Formenherstellung benötigt?
Der Lieferant sollte das 3D-Modell, das Material, das voraussichtliche Jahresvolumen, die Anforderungen an das Erscheinungsbild, die Toleranzanforderungen sowie etwaige Anforderungen an die Montage oder Funktionsprüfungen bestätigen.
What is the biggest risk in Two-Shot Molding vs Overmolding — Multi-Material Processing Guide?
Das größte Risiko besteht darin, die Werkzeuge freizugeben, bevor das Materialverhalten, der Schwund, der Fließverhalten und die Funktion des Bauteils im Hinblick auf die tatsächliche Anwendung vollständig überprüft wurden.
What should a two-shot injection molding quote clarify before tool design?
Provide both material grades, hardness and color, the complete assembly, bond or seal areas and cosmetic boundaries. Define the production quantity and how adhesion, dimensional fit and leakage will be accepted. Ask the quote to identify tooling, transfer or rotation, material compatibility trials and inspection, and compare insert overmolding or separate assembly where those routes satisfy the same requirement.
Weiterführende Lektüre
- Leitfaden zu den Drucktemperaturen für Nylon
- CNC-Bearbeitung von Nylon
- 3D-Druck für Prototyping und Produktion
- Leitfaden zur Auswahl von Kunststoffmaterialien
- Kostenfaktoren für technische Kunststoffe
- Nylon-Spritzguss: Vollständiger Leitfaden für das Multi-Material-Spritzgießen
- Nylon-Spritzguss: Verarbeitungsparameter und Fehlerbehebung