
Warum importierte Kunststoffteile ein strukturiertes Qualitätsmanagement erfordern
Quality inspection for imported plastic parts works best when the buyer and supplier agree what must be approved before the order is placed. Define the drawing revision, exact material, critical characteristics, measurement condition, sampling plan and required records. FAI, PPAP and incoming inspection answer different questions; receiving a shipment does not replace production approval.
Make the Acceptance Scope Part of the Quotation
Send the drawing, material requirement, quantity, cavity coverage and customer reporting template with the part RFQ. Nylon Plastic can review material and manufacturing needs together with the inspection scope to quote. Identify any independent laboratory or third-party inspection work separately rather than assuming it is included.
Erstmusterprüfung: Die Grundlage der Qualitätssicherung
First article inspection links production-representative samples to the released drawing and approval requirements. Agree the characteristics to report, sample selection, cavity coverage, production condition and acceptance authority. A first sample result is useful evidence; it is not by itself proof of long-term process capability.
Use a numbered or ballooned drawing so each result can be traced to a dimension, note, material or functional requirement. Record actual values where applicable, the method, instrument, inspection condition and pass/fail conclusion. Identify cavities separately when they can influence the result. Sample count and production stabilization criteria belong in the project inspection plan, rather than a universal number of shots or parts.
| FAI item | Agree before sampling | Evidence to return |
|---|---|---|
| Drawing and revision | Features, datums, tolerance and appearance acceptance | Characteristic number, specification and actual result. |
| Cavity coverage | Required parts from each relevant cavity and sampling conditions | Sample/cavity identity linked to dimensional results. |
| Material and condition | Offered grade, color, reinforcement and inspection state | Supplier documents and any agreed material tests. |
| Functional approval | Assembly, load, seal or other application checks | Method, conditions, result and unresolved deviations. |
PPAP-Einreichungsstufen für Kunststoffteile
PPAP is a customer-defined production approval submission, often used in automotive programs. A dimensional report may be one element within a broader package of process and material evidence. Confirm the applicable customer manual, submission level, forms, retention requirements and approval authority before quoting the work.
Do not assume every plastic-part order requires the same PPAP level or that a general FAI report completes PPAP. Provide the customer requirements and identify what records must be submitted, what must be retained and any specialist testing involved. The quote should state the agreed package and any items requiring further review.
Verfahren zur Maßprüfung von Kunststoffteilen
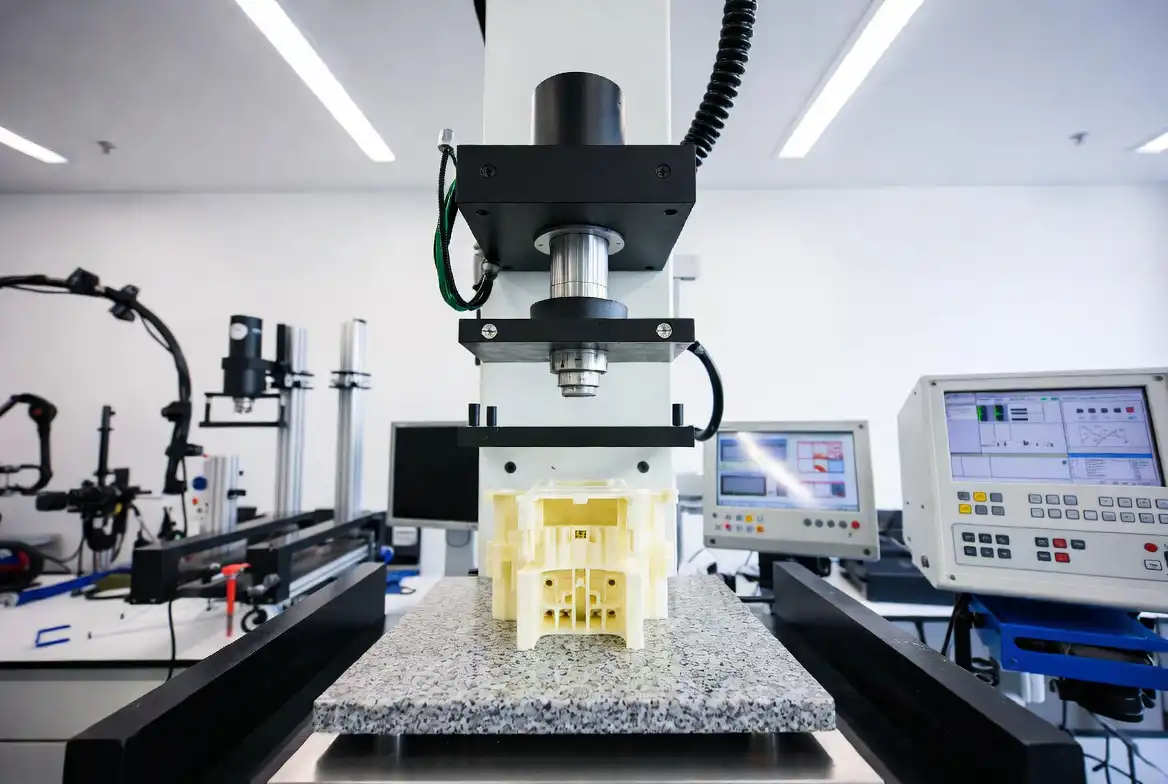
Choose the measurement method for the feature and required confidence, rather than using one instrument for the entire part. Calipers or gauges may suit accessible simple features; CMM or optical methods can help evaluate geometry and feature relationships. Hidden structures may require a specialist method. None of these instruments is proof that a specific inspection service is included.
Plastic parts can deform under clamping or contact forces. Define datums, fixture, measurement force where relevant, temperature, moisture state and stabilization procedure. Use the drawing, material behavior and applicable test requirements to set conditioning; a fixed four-hour wait does not establish moisture equilibrium for every polymer or geometry.
| Feature or question | Method to review | Important limitation |
|---|---|---|
| Accessible diameter, length or thickness | Suitable calibrated gauge, micrometer or caliper | Contact force, access and datum definition. |
| Complex shape or position | CMM, optical or scanning method | Fixture condition, measurement strategy and method validation. |
| Hidden structure or internal defect | Specialist CT or another validated method | Technical suitability and supplier/laboratory scope must be agreed. |
| Assembly or sealing | Application-specific fit or functional test | Passing isolated dimensions does not establish assembly performance. |
Materialzertifizierung: CoA, CoC und unabhängige Überprüfung
Identify the material manufacturer, exact grade and lot associated with the supplied parts. A CoA reports the tests the issuer actually performed for the identified lot; a CoC states conformity within its stated scope. Read the document, specification and traceability together. Neither title guarantees that every property on the project specification has been tested.
Independent tests can answer specific material questions, but they have limits. FTIR can support polymer-family identification; thermal or compositional analysis may help investigate fillers or material behavior. A matching family result does not prove an exact commercial grade, additive package or certification. Agree the laboratory, method, reference material, scope and interpretation before testing.
Manufacturer documents retain their manufacturer attribution. If a WanHan datasheet is used for a material review, WanHan is identified as manufacturer; the offered grade and relevant batch evidence still need to match the order.
Funktionsprüfung von Kunststoffteilen
Define functional checks from the application: mating-part fit, insert retention, snap-fit force, leakage, load, temperature cycling, fluids or weather exposure may matter. Specify the method, conditions, duration, sample count and acceptance criteria. A universal low-temperature limit or test sequence is not suitable for every project.
Agree which tests the supplier, buyer or independent laboratory will perform and which results must be included in the approval package. An appearance sample, resin datasheet or dimensional report does not replace an application-specific functional test.

Normen für Oberflächenbeschaffenheit und Prüfung
Specify the required finish or texture reference, color and appearance zones. If a VDI or SPI reference is used, identify the exact grade/reference and the agreed acceptance sample. Polymer, filler, color and process conditions can affect the appearance produced by the same tool texture.
For visual acceptance, agree lighting, viewing distance and angle, permitted marks and limit samples where useful. Where roughness is a functional requirement, define the measurement method and tolerance separately. Avoid treating a generic texture-to-roughness conversion or an ideal photograph as approval of the supplied part.
Fehlerklassifizierung und AQL-Stichprobenverfahren
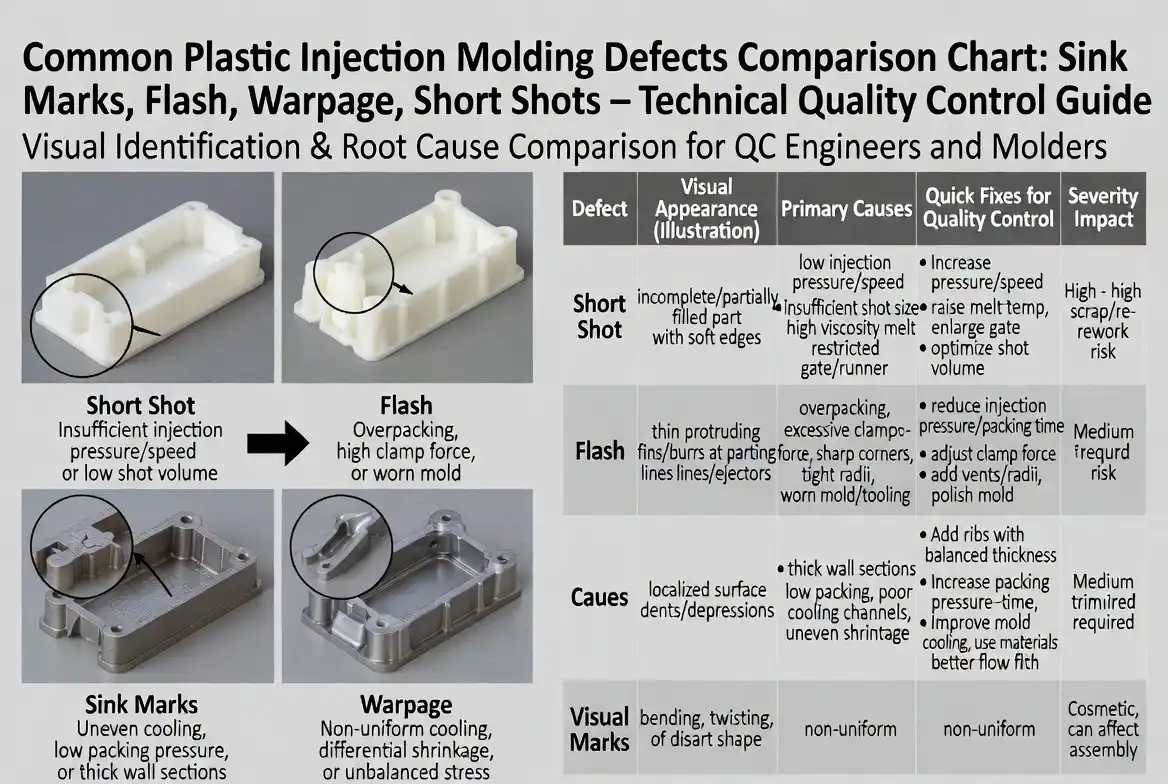
Define defects by the consequences for your part. Critical, major, minor and cosmetic categories must have agreed examples and disposition rules. Cosmetic appearance can be a major requirement for some products; a crack or flash cannot be classified solely by its name without the function and drawing context.
Choose the sampling scheme, standard and edition, lot size, inspection level, acceptance/rejection criteria and switching rules before production. AQL-indexed sampling is a defined system, not a universal acceptable defect percentage for every shipment. A zero-acceptance rule does not establish that every item in the lot is defect-free. Confirm appropriate controls for critical requirements with the responsible quality team.
| Anforderung | What to agree | Record in the report |
|---|---|---|
| Critical characteristics | Detection/control method and no-acceptance or other required rule | Actual checks, findings and responsible disposition. |
| Major/minor defects | Definitions, examples and the approved sampling plan | Counts by agreed category and acceptance/rejection decision. |
| Aussehen | Visible zones, reference samples and inspection conditions | Defect location, image and comparison against the agreed limit. |
| Nonconforming lot | Containment, sorting, rework or return and approval authority | Hold/release decision and required correction or reinspection. |
Prüfdienstleistungen durch unabhängige Dritte
Independent inspection can support supplier review, checks during production, pre-shipment inspection or receiving decisions. Define when the goods are available, what lot and packing status can be sampled, what tests are possible on site, and what specialist work needs another laboratory.
The scope should identify drawing and sample references, quantity, sampling plan, measurement and functional checks, packaging/labeling and the report required. Fees and timing depend on location, access, duration and test scope; request them from the selected inspection provider rather than relying on a generic day rate. An independent inspection does not replace an agreed supplier approval or customer acceptance requirement.
Vorlage für Inspektionsberichte und Dokumentation
Ein standardisierter Prüfbericht erfasst alle Befunde in einem Format, das die Erstellung von Trendanalysen, Lieferanten-Scorecards und die Anforderungen an den Prüfpfad unterstützt. Der Bericht sollte die Teilenummer und Revision, den Namen des Lieferanten, die Bestellnummer, die Los- oder Chargennummer sowie das Datum der Prüfung enthalten. Der verwendete Stichprobenplan, einschließlich Losgröße, Stichprobengröße, Prüfstufe und AQL, muss angegeben werden. Bei Maßergebnissen sollte jedes Merkmal durch die Ballonnummer aus der Zeichnung, die Spezifikation und Toleranz, die tatsächlichen Messergebnisse mit dem verwendeten Messgerät sowie eine Bewertung als „bestanden“ oder „nicht bestanden“ identifiziert werden. Bei der Sichtprüfung sollte das Fehlerklassifizierungssystem angewendet werden, wobei die Anzahl der jeweils festgestellten Fehlerarten und der AQL-Vergleich anzugeben sind. Der Status der Materialzertifizierung, einschließlich der Überprüfung des CoA und etwaiger unabhängiger Prüfergebnisse, sollte dokumentiert werden. Eine klare Gesamtentscheidung über die Chargenverwendung (Annahme, Ausschuss oder Sortierung und Nachbearbeitung) sollte unter Angabe des Namens und der Unterschrift des Prüfers festgehalten werden.
Der Prüfbericht ist nicht nur ein Dokument zur Einhaltung von Vorschriften. Er ist ein Managementinstrument. Die Analyse von Trends bei den Fehlerarten über verschiedene Chargen hinweg deckt systematische Prozessprobleme beim Lieferanten auf. Die Verknüpfung der Ergebnisse der Wareneingangskontrolle mit Problemen in der Produktionslinie liefert Rückmeldung darüber, ob die Prüfkriterien angemessen sind. Der Austausch von Prüfdaten mit dem Lieferanten im Rahmen eines strukturierten Qualitätsrückmeldungsprozesses fördert die kontinuierliche Verbesserung und senkt im Laufe der Zeit die Prüfkosten, da nachgewiesene Leistungsfähigkeit eine Reduzierung der Stichproben oder den Übergang in den „Dock-to-Stock“-Status ermöglicht.

FAI vs PPAP vs Incoming Inspection: Define the Approval Gate
First article inspection for plastic parts verifies that the released drawing, resin, mold, cavity and approved process can produce every specified characteristic. PPAP is a broader production-approval package that may include FAI-type dimensional results plus process flow, control plan, PFMEA, material evidence, capability data and customer-specific forms. Incoming inspection is a receiving-control activity; it does not replace supplier process approval.
| Activity | Primary Question | Typical Evidence | Repeat Trigger |
|---|---|---|---|
| FAI | Does the first production-representative output meet the drawing? | Ballooned drawing, actual dimensional results, material and functional evidence | New or changed tool, cavity, drawing, material, site or significant process |
| PPAP | Can the complete production system repeatedly meet requirements? | Customer submission level, control plan, PFMEA, capability and samples | Customer rules and significant product or process change |
| Incoming QC | Does the received lot meet the agreed acceptance plan? | Sampling record, visual/dimensional results and lot disposition | Each lot or risk-based frequency |
Ballooned Drawing and Characteristic Accountability
Every note, material callout, dimension, GD&T control, cosmetic zone and functional requirement should receive a unique balloon number. The report must map that number to the specification, actual result, method, instrument and pass/fail status. Record values rather than only writing OK wherever variable data is practical. Each cavity should be identifiable because pooled samples can hide a cavity-specific dimensional shift.
When FAI Must Be Repeated
Repeat or partial FAI is normally considered after a drawing revision, resin or colorant change, mold repair, cavity addition, tool transfer, long production interruption, significant process change, or a corrective action affecting fit or function. Buyer and supplier should agree which characteristics are affected instead of assuming that either a full resubmission or no resubmission is always correct.
Buyer Review and FAI RFQ Checklist
- Controlled drawing and CAD revision with balloon numbering.
- Production-intent resin grade, colorant, mold, cavity and process.
- Sample quantity and required coverage for every cavity.
- Dimensional, material, cosmetic and functional evidence.
- Measurement method, conditioning, fixture and instrument traceability.
- Clear deviation, concession, approval and resubmission rules.
For detailed method selection, see our plastic parts inspection and metrology guide.
Häufig gestellte Fragen
Was ist der Unterschied zwischen FAI und PPAP?
FAI compares production-representative output with the agreed drawing and other approval requirements. PPAP is a broader customer-defined submission that may include dimensional results, process controls, material evidence and other required records. Incoming inspection checks the received lot; none of these activities automatically replaces the others.
Wie berücksichtige ich die Schrumpfung von Kunststoffteilen bei der Festlegung der Prüfmaße?
Inspect against the released final-part drawing, using its agreed datums, conditions and method. Tool shrinkage compensation is reviewed in tool design; it is not added to the acceptance dimensions. Define temperature, moisture state and stabilization according to the grade, geometry and applicable requirements, and record those conditions.
Was ist ein angemessener AQL-Wert für Kunststoffspritzgussteile?
There is no single setting for every part or industry. Agree the defect categories, relevant standard and edition, lot size, inspection level, plan and acceptance/rejection criteria with the responsible quality team. Include the chosen plan in the order or quality requirements.
Wie kann ich überprüfen, ob der Kunststoff meiner Teile den Spezifikationen entspricht?
Review the offered manufacturer and grade, lot traceability and the scope of CoA or CoC evidence. If uncertainty remains, agree targeted independent testing and its interpretation. Polymer-family identification alone does not prove an exact compound grade or every required property.
Sollte ich die Ware im Werk des Lieferanten oder bei Erhalt der Lieferung prüfen?
Beides, allerdings zu unterschiedlichen Zwecken. Durch die Prozess- und Vorversandkontrolle im Werk des Lieferanten werden Mängel bereits vor dem Versand erkannt, wodurch die Frachtkosten für fehlerhafte Teile gesenkt und der Korrekturzyklus verkürzt werden. Die Wareneingangskontrolle in Ihrem Werk bestätigt, dass die Teile nach dem Transport den Spezifikationen entsprechen, und bildet die Grundlage für Ihre endgültige Abnahmeentscheidung. Bei kritischen Programmen bietet eine Kombination aus Lieferanten- und Prozessaudit, Inspektion vor dem Versand und Stichprobenprüfung bei Wareneingang den umfassendsten Qualitätssicherungsschutz.
Weiterführende Lektüre
- So überprüfen Sie einen chinesischen Kunststoffhersteller
- RoHS and REACH Compliance for Plastic Parts Export
- Leitfaden zur Versand- und Importlogistik für Kunststoffteile
References: ISO 291 conditioning and testing scope, ISO 2859-1:2026 sampling-system scope, und ZEISS plastic first-article metrology guidance. Agree the applicable customer requirements and standard edition for your project; specialist methods described by manufacturers are not claims of Nylon Plastic equipment ownership.
Request a Plastic Part and Quality Inspection Scope Review
Senden: drawing/CAD revision, material grade, order quantity, cavity coverage, critical dimensions, appearance reference and the required report or customer template. Include service conditions and delivery destination when these change acceptance.
The review can clarify: material and manufacturing options, the inspection records to include in the quotation, sample approval responsibilities and any tests requiring a separately agreed provider. Use this for a material or part project rather than assuming a standalone independent inspection is included.